Blog

  • ISR Sync Test Post From Ego

    This article was created end-to-end by an automated browser agent in the WordPress block editor. It exists to verify that publishing a native WordPress Post propagates to the Next.js front end.

    What this test verifies

    The block editor writes a native Post, the CMS marks it approved, and the front end should serve it without a rebuild.

  • Native Post Media Import Verification

    Media import verification

    This local article checks whether WordPress media reaches the native Post contract and the Next.js presentation layer.

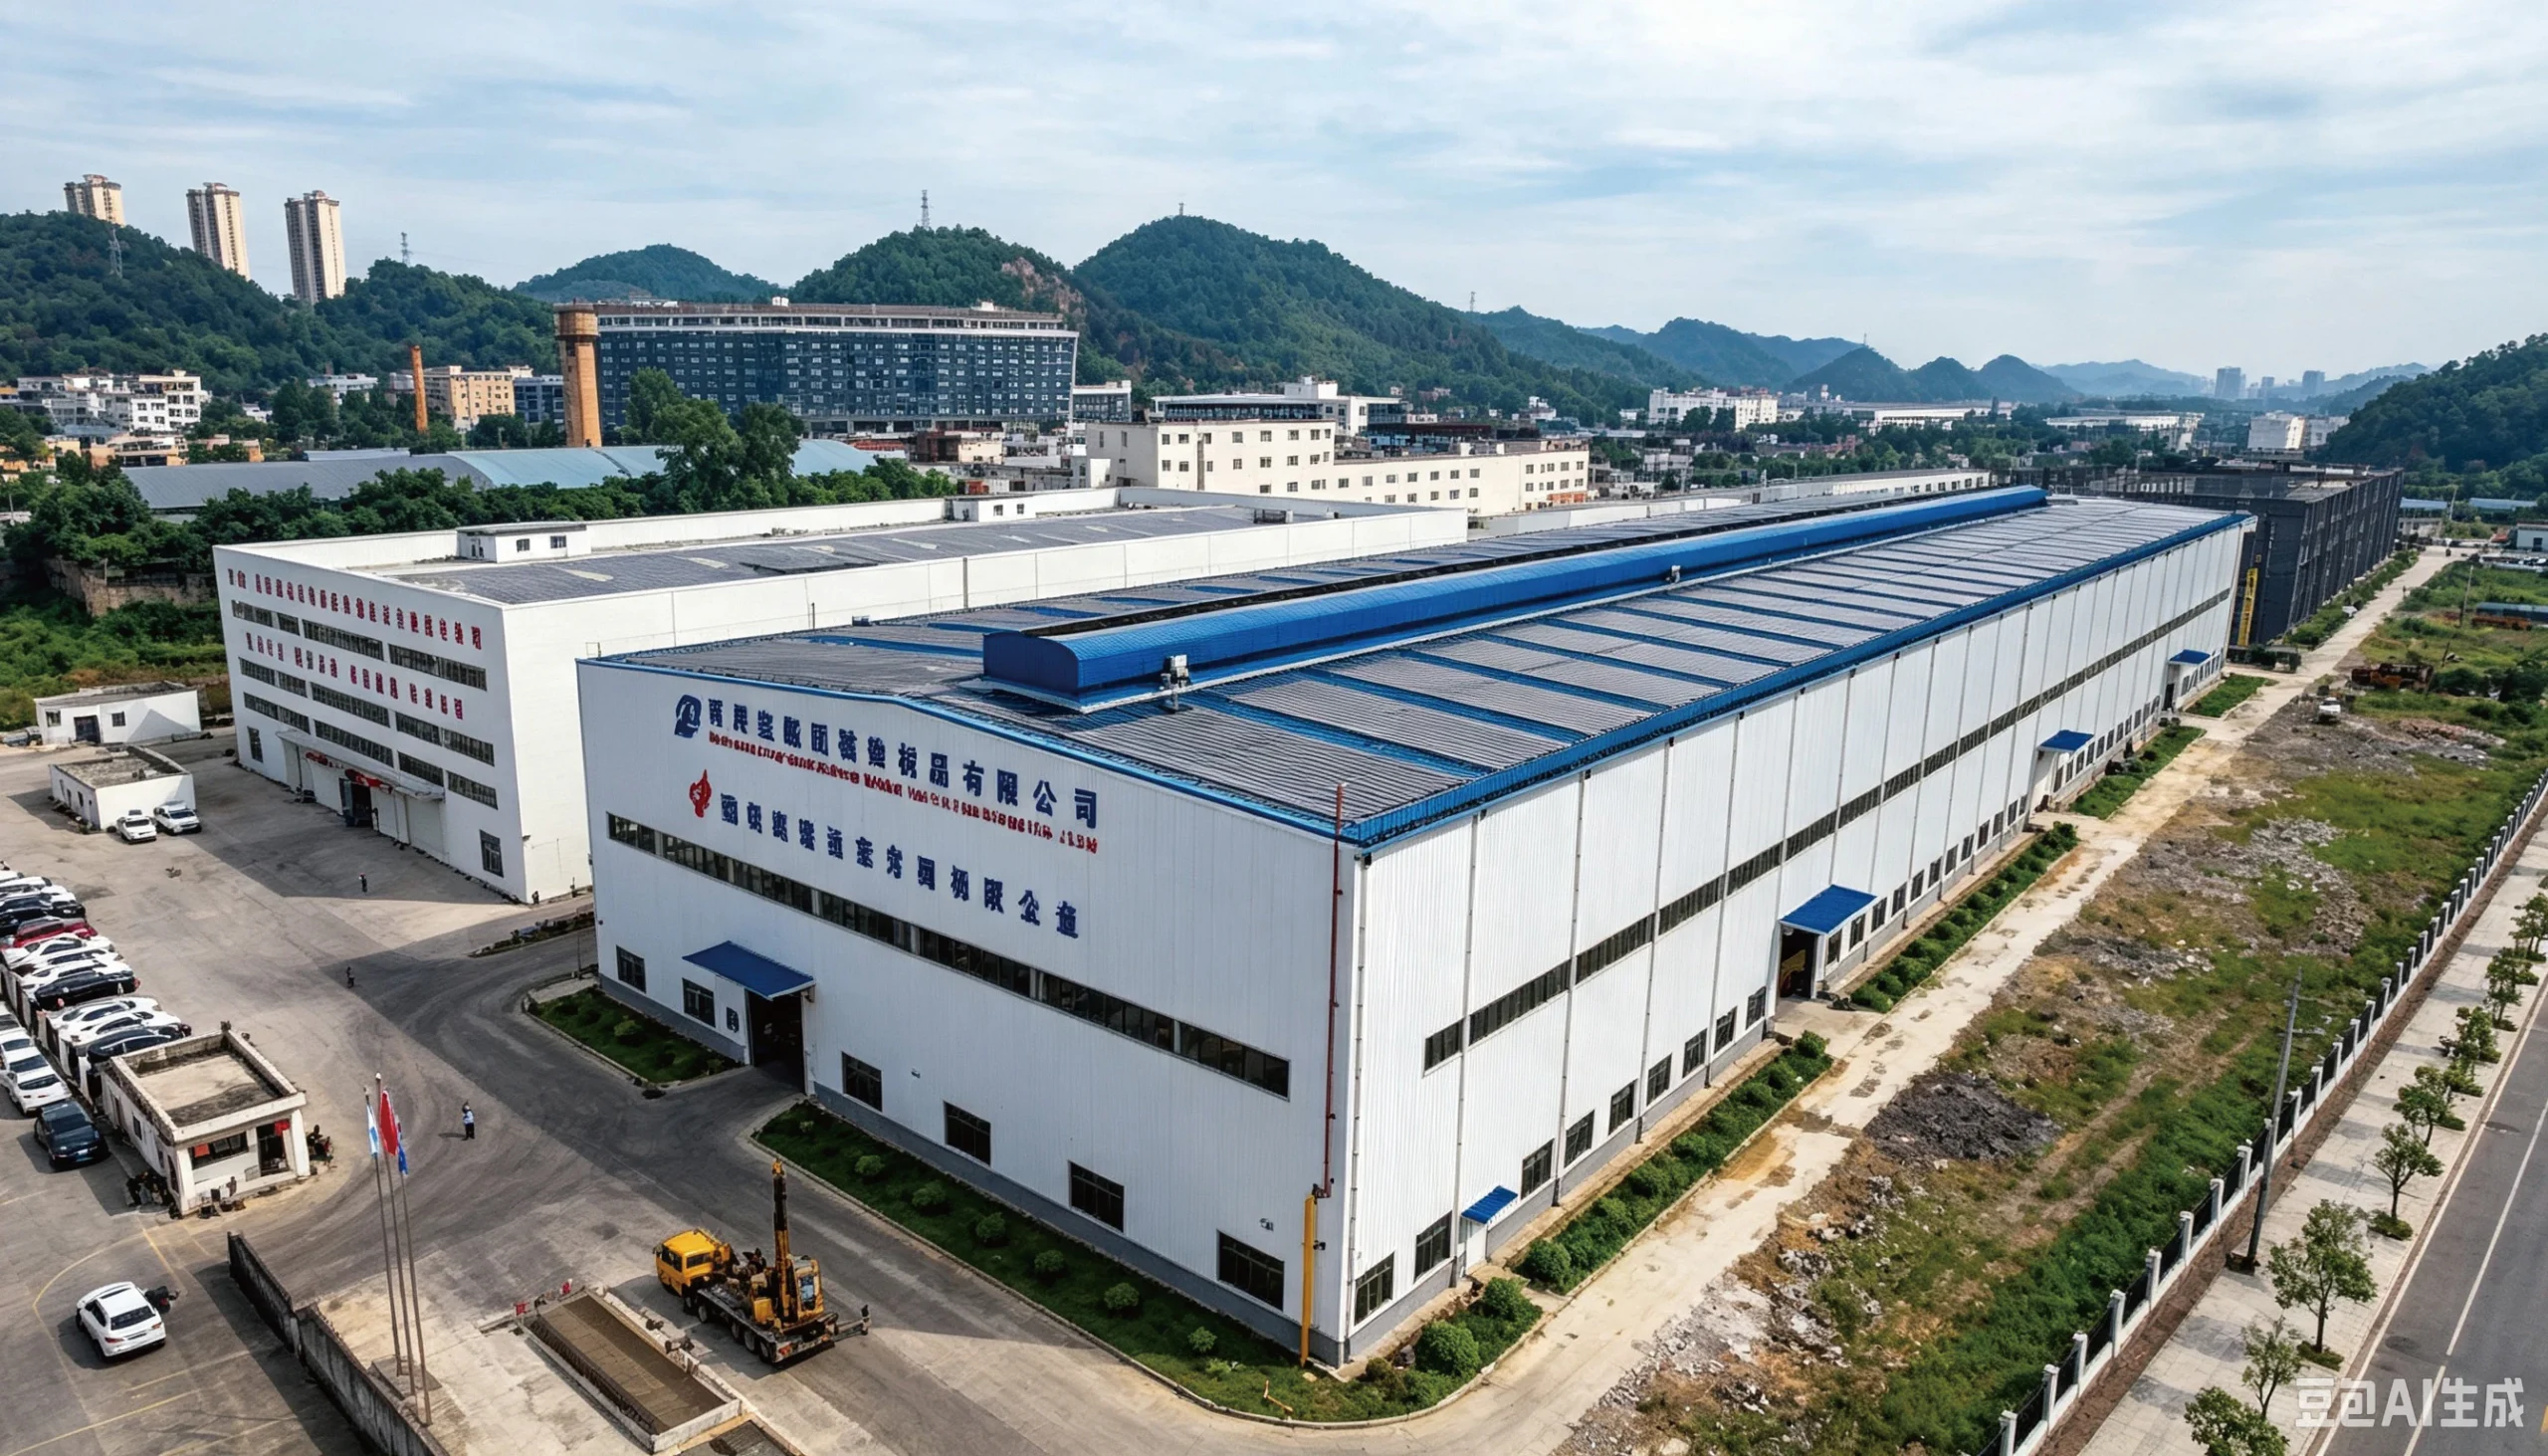
    Aerial view of a Fenghuai manufacturing facility
    Commercial and shipping terms are confirmed for each destination market.

    The image above is a local media-library asset with an attachment ID, source URL, alternative text and caption.

    Expected result

    The featured image should appear in the article hero. Body-image rendering is included as a compatibility probe for the current content contract.

  • Native WordPress Post Authoring Test

    What this local test verifies

    This article verifies the native WordPress Post workflow, the Gutenberg content seam, structured fields, the REST contract, and the Next.js rendering path.

    • Native Post is the only authoring entry.
    • Gutenberg content is filtered by WordPress before delivery.
    • Structured metadata remains available through the stable guide contract.
      • Legacy JSON remains a rollback path.

    Approved content should pass through one stable contract before it reaches the page.

    Read the local Insights index or the WordPress editor documentation.

    Result

    The article is intentionally marked as a local acceptance record. It contains no production product claim and can be removed after review.

  • Importing wheels: freight and duties

    The landed cost is not the invoice price

    The number a dealer needs before quoting a customer is the landed cost: the price of the goods plus freight, insurance, duty, and any clearance and handling charges to the point of delivery. Quoting from the invoice price alone is how a job that looked profitable turns out not to be.

    The size of that gap depends on the destination market and on the terms agreed, so it has to be calculated per shipment. A rate that applied to a previous order to a different market is not evidence of anything.

    Agree the incoterm first

    The incoterm — the three-letter trade term — decides where responsibility passes from seller to buyer. It determines who arranges and pays for freight, who arranges insurance, who clears the goods and who pays the duty.

    The practical consequence is that two identical invoices can have very different landed costs depending on the term. FOB, where the buyer takes responsibility once the goods are on board, is a different commercial deal from DDP, where the seller delivers to the buyer's premises with duty paid.

    This has to be agreed before a price is given to the end customer. A dealer who quotes a customer on one basis and then discovers the shipment was agreed on another has lost the difference out of their own margin.

    PLACEHOLDER: confirm which incoterms Fenghuai offers, which it declines, and produce a short dealer-facing explanation of each before this advice is published.

    Classification, origin and the invoice

    Every consignment needs a correct HS classification — the harmonised system code that tells customs what the goods are — and a stated country of origin. Both appear on the commercial invoice, and both need to be right.

    A wrong description is not a minor clerical issue. It stops the consignment at the border while it is queried, which usually happens at the worst possible moment for the customer waiting on a set of wheels. Resolving it takes time you did not plan for and delays you cannot explain away.

    Duty rates vary by destination and by classification, so the correct rate has to be looked up for the specific market rather than carried over from another shipment. VAT or sales tax treatment likewise varies by destination.

    Packing, and why it decides your claim

    Wheels are heavy and awkward to handle. Once a pallet is in a freight network it is moved by machinery, loaded and unloaded several times, and stacked against other freight. Packing that would be fine for a courier parcel is not adequate for international freight.

    Freight-grade packing — reinforced corners, wheels separated from each other, the pallet itself secured — costs less than the damage claim it prevents. A claim is also slow: even where it succeeds, the customer is waiting while it is resolved.

    Documentation is what decides a claim. Photograph the consignment before it leaves and again on arrival, and keep the inspection record with the shipment paperwork. A claim without evidence of the condition at dispatch is much harder to substantiate.

    A pre-shipment checklist

    Before any order ships, confirm: the incoterm is agreed and in writing; the invoice states the correct HS classification and country of origin; freight and insurance are arranged on the agreed basis; the packing meets a freight standard rather than a parcel standard; and photographs and the inspection record are captured before the goods leave the facility.

    PLACEHOLDER: which of these Fenghuai performs, and which sit with the dealer, must be confirmed and documented internally before this checklist is presented to dealers as fact.

  • Finishing options explained

    Two attributes, not one

    A finish is a combination of a surface treatment and a colour. Surface treatment describes how light behaves when it hits the metal: whether it is scattered evenly by a matte or satin texture, reflected sharply by a polish, or caught in fine lines by a directional brush. Colour describes the hue that the treatment is applied over or tinted with.

    These are independent. Satin black and gloss black are the same colour with different surface behaviour. Satin bronze and gloss bronze likewise. When a customer describes the finish they want, establishing which of the two they are actually reacting to — the texture or the hue — resolves most of the ambiguity before it becomes a dispute.

    The common surface treatments

    Brushed finishes apply a fine directional grain to the metal under a clear coat. The grain catches light differently as the wheel turns, so a brushed wheel changes character with the angle you view it from. It reads as technical and understated.

    Polished finishes reflect sharply and show a hard highlight where they catch the light. On a rim lip, a polish draws an edge line around the wheel; on a full face it is a much stronger statement and needs more care to maintain.

    Satin sits between matte and gloss: a soft sheen without a hard reflection. It is the most forgiving of the gloss levels against most body colours.

    Matte scatters light evenly and shows no reflection. It is understated and it hides minor surface variation well. The trade-off is that matte surfaces can be harder to clean uniformly, since some cleaning products leave a sheen behind.

    Gloss is fully reflective, hardest and easiest to wipe clean, and provides the maximum contrast and depth. It is also the least forgiving of surface defects, because a reflection shows every imperfection.

    Colour, and the problem with swatches

    A flat colour swatch is a representation, not a sample. It cannot show how a directional grain behaves as the wheel rotates, how a gloss reads in direct sunlight versus shade, or how the finish interacts with the specific paint on the car it will sit on.

    On top of that, screens render colour differently from each other and from the real object, and a swatch seen on a phone is not evidence of what a delivered wheel will look like. For anything other than a straightforward gloss or matte black, a physical sample or a photograph of the exact finish on an actual wheel is worth the effort before a customer commits.

    Note also that a two-tone finish is not one colour — it is two, usually a contrasting face and lip. Those need to be agreed together, because the contrast is the point.

    Repeatability is the real risk

    The first order is rarely the problem. The second order, six months later, is. Finish repeatability depends on controlled process stages: consistent surface preparation, consistent application, consistent curing. Where those vary, the second batch will not match the first, and a customer who ordered one wheel to replace a damaged one will notice immediately.

    The mitigation is record-keeping. What matters is not what the finish was called on the invoice but what was actually applied and how. When a repeat order comes in, we should be able to reproduce the previous process, not approximate it from a name.

    How to specify a finish without problems

    Agree the colour and the surface treatment as two separate decisions. If the finish is anything other than a basic gloss or matte, get a physical sample or a photograph of the exact finish on a wheel in front of the customer before the order is placed. Record what was supplied, not just its name, so the next order can be matched.

    PLACEHOLDER: confirm which finishes Fenghuai currently offers, and produce a sample policy stating what we will send and how fast, before publishing this guide as advice.
  • How to measure your fitment

    The five numbers a wheel order is built from

    Every forged wheel is manufactured to five values. Diameter and width define the size. Offset defines where the wheel's mounting face sits relative to its own centreline. PCD — the bolt pattern — defines the circle the mounting holes sit on and the number of studs or bolts. Centre bore defines the hub hole that centres the wheel on the vehicle.

    Two of these are visible to anyone: diameter and width. They are also the two that customers lead with, which is why they get the most attention and cause the least trouble. The other three are effectively invisible on a finished car, and they are where orders fail.

    The important thing to understand is that these are not independent. Change the width and you change where both edges of the wheel sit for a given offset. Change the offset and you move the whole wheel in or outboard without changing its width. A specification that quotes a width but not an offset is not a specification — it is half of one.

    Why a tape measure alone is not enough

    It is tempting to measure the gap between the current wheel and the arch, add that as additional width, and quote the result. That works on the outboard side and tells you nothing about the inboard side, which is usually the real constraint.

    The inboard lip has to clear the suspension strut, control arms, brake caliper and any brake cooling ducting. On a car with a large brake package, that clearance can already be tight with the factory wheel. Add width on the outboard side by reducing offset and you have simultaneously moved the inboard lip closer to those components.

    This is why we start from the OEM specification for the exact trim rather than from a measurement. The OEM number is a known-good baseline that clears everything as shipped. Adjustments from there are deliberate and can be checked one at a time.

    Reading offset off a wheel you have in front of you

    Offset is normally stamped or cast on the inside of the wheel, usually as an ET number. Where it is not legible, you can measure it: lay the wheel face-down on a flat surface, measure the distance from the mounting face down to the surface — that is backspacing — then relate it to the wheel's width.

    Backspacing and offset describe the same geometry from opposite ends, and you cannot convert between them without knowing the width. That conversion is covered in its own guide, because confusing the two is a common cause of a mis-quoted fitment.

    PCD and centre bore: measure, do not guess

    Both are easy to measure incorrectly and both matter. PCD is the diameter of the circle passing through the centre of the bolt holes — not the distance between two adjacent holes, which is the mistake people make and which gives a plausible-looking wrong answer. Centre bore is the diameter of the hub hole and must match the vehicle's hub spigot.

    We do not recommend spigot rings as a way to bridge a centre-bore mismatch on a custom order. If we are manufacturing the wheel for your car, the correct answer is to build it with the right centre bore in the first place.

    What we need from you to confirm a fitment

    Send the vehicle make, model, exact trim and model year, the chassis code where you know it, the brake package if there is more than one, any suspension change, and the stance you are targeting. If you have the OEM wheel specification, include it.

    We will review that against the clearance envelope and the load rating, propose a specification, and return it to you in writing for approval before anything is cut.

    PLACEHOLDER: any specific measurement value quoted to a customer — offset, PCD, centre bore, or a load rating — must come from Fenghuai engineering for the specific vehicle. Nothing on this page should be used as a lookup value.

  • Understanding offset and backspacing

    Two reference points, one geometry

    Offset is measured from the wheel's own centreline to its mounting face. Positive offset means the mounting face is outboard of the centreline — the wheel's mounting surface sits closer to the outside face. Negative offset means the mounting face is inboard of the centreline.

    Backspacing is measured from the mounting face to the inboard edge of the wheel. It is a different question: not 'where is the face relative to the wheel' but 'how far does the wheel reach inboard once it is bolted on'.

    Both are correct descriptions of the same wheel. Which one you use depends on the question you are asking. If you are comparing wheel designs against each other, offset is natural. If you are asking whether a wheel will clear the suspension, backspacing is the more direct answer.

    The conversion, and why width is mandatory

    Because offset is measured from the centreline and backspacing from the mounting face, converting between them depends on where the mounting face sits relative to the centreline — which is exactly what offset describes — and on the total width, which is what tells you where the inboard edge is.

    So the conversion requires both values. A specification that gives backspacing but omits the width cannot be converted back to an offset, and a specification quoting offset without a width cannot tell you whether the inboard lip clears anything.

    The practical rule: never accept a fitment figure in isolation. A useful fitment specification states diameter, width, offset, PCD and centre bore together.

    Where each one actually decides the outcome

    The outboard question — does the wheel sit flush, tuck, or poke — is an offset question, because it is about where the outer face lands relative to the arch.

    The inboard question — does the wheel foul the strut, the arm or the caliper — is a backspacing question, because it is about how far the wheel reaches inwards from the mounting face.

    Most fitment failures we see are inboard. A wheel that looks perfect against the arch can still catch a control arm on compression, and that is not something you can assess by eye from outside the car. On a car with a large brake package, the margin is often already small with the factory wheel.

    Negative offset and the brake problem

    Aggressive negative offset pushes the wheel outboard, which reduces the space available on the inboard side. On a car with a big-brake option, that space is already the tightest part of the whole envelope.

    The consequence is that a low-offset wheel that fits a car with standard brakes may not clear the same car optioned with the larger brake package. This is why we ask for the brake option, not just the model.

    How we work it out for you

    Agree the target stance first. That is a customer decision and it should be made deliberately, not arrived at by accident from a wheel that happened to be available.

    We then work back to an offset that delivers the stance without consuming the clearance you need on the inboard side, and return the resulting specification — with all five values — in writing before the order is cut.

    PLACEHOLDER: any specific offset or backspacing value we quote must be produced by Fenghuai engineering for the specific vehicle. Do not treat numbers from this guide as buildable specifications.

  • Monoblock vs two-piece: choosing a construction

    What each construction actually is

    A monoblock wheel is machined from a single forged blank. The spoke face, the rim and the mounting pad are one continuous piece of metal. There is no interface, no bolts and no seal between two parts.

    A two-piece wheel has a forged centre — the face and spokes — mated to a separately formed barrel that supplies the rim and the lip. The two are joined and sealed. Because the centre and the barrel are manufactured independently, each can be shaped for its own purpose: the centre for the spoke design, the barrel for lip depth and width.

    That separation is the whole point. It is what allows a deep lip to exist independently of the face design, and it is what allows barrel widths that a single machined piece cannot economically reach.

    The performance case for monoblock

    Removing the joint and its hardware removes mass, and it removes a set of fastened interfaces that all have to stay tight over the life of the wheel. For a wheel that is expected to be light and to stay true, a single piece is the cleaner engineering answer.

    The practical benefit is unsprung and rotational mass. Reducing either improves how a car responds — steering feel, ride quality over sharp inputs, and the effort the suspension has to control. This is directionally true on any car and most noticeable on a performance platform.

    We deliberately do not quote specific weight savings in this guide. Any figure quoted to a customer should come from our engineers with a stated test basis for the exact specification being ordered.

    The case for two-piece

    Two-piece exists to solve problems monoblock cannot. If the requirement is a deep lip, or a step-lip profile that sets the rim depth visually as well as physically, that is a two-piece answer. If the requirement is a width beyond what a monoblock blank can be machined to at that diameter, that is also a two-piece answer.

    The second benefit is serviceability. A barrel that is damaged can be replaced without discarding the forged centre. On a wheel that lives on a track car or a car parked regularly against kerbs, that is a real reduction in the cost of ownership over several years.

    How to choose, in order

    First, establish the hard constraint. Is there a width or lip depth the customer needs that monoblock cannot produce? If yes, the decision is made for you and the conversation moves to which two-piece configuration delivers it.

    Second, if both are viable, ask what the customer actually values. Unsprung weight and stiffness point to monoblock. A specific lip look, or the ability to replace a barrel later, points to two-piece.

    Third, be honest about the trade. If a customer is chasing lap-time feel and asks for a deep lip because they saw one they liked, the correct advice is that the two objectives pull against each other and they should choose which one matters more.

    What we need from you

    Tell us the vehicle, the width and diameter target, the stance, and what the customer values most. We will tell you which construction is buildable for that requirement and, where both are, what the trade-off looks like in practice.

  • Forged vs cast wheels

    The manufacturing difference

    Casting and forging are different ways of turning aluminium alloy into a wheel. Casting pours molten metal into a mould shaped like the finished part. It is efficient, it allows complex shapes, and it is the reason a cast wheel can be affordable.

    Forging takes a solid billet and works it under high pressure into the rough shape of the wheel, before machining refines it. The pressure deforms the metal rather than melting it, and that process aligns the material's internal grain structure to follow the form of the part.

    The difference that matters is not a single number, it is the directionality and the consistency of the material. A forged part has a grain that runs with the load paths. A cast part has a grain structure determined by how the metal cooled, which is generally less directional and more likely to include internal porosity.

    What that gives the driver

    Because forged material is doing more work per unit of mass, a forged wheel of a given size and strength can generally be built lighter than an equivalent casting. The benefit is unsprung and rotational mass: less weight for the suspension to control, less inertia for the drivetrain to spin up.

    The other benefit is toughness. On a truck or SUV that sees rough surfaces, the resistance to impact damage and the ability to carry load matter more than lap-time feel. Forging helps there too.

    We deliberately do not publish specific strength or weight figures in this guide. Where a customer needs numbers, they should come from our engineers with a stated test basis and for the exact specification being ordered.

    The cost, stated plainly

    Forging costs more. The billet is more expensive than the raw material for a casting, the forging process itself is capital-intensive, and removing material from a solid forged blank by machining takes longer than finishing a casting near its final shape.

    That cost is real and it does not disappear through scale. A dealer quoting a forged wheel against a cast competitor is quoting a different product, and the honest framing is to explain what the customer is buying rather than to try to match the cast price.

    When cast is a legitimate recommendation

    If the customer's budget or use case does not support a forged wheel, saying so is better than stretching the truth. A cast wheel sold as a cast wheel sets the right expectation; a cast wheel implied to be forged does not, and it comes back as a complaint the first time something goes wrong.

    There are applications where a forged wheel is genuinely not the priority: a low-mileage show car, a spare, or a winter set. In those cases a well-made cast wheel can be the correct answer, and recommending it honestly is how you keep the account.

    What we need from you

    Tell us how the car is used, what the customer values, and what the budget allows. We will recommend a construction and be explicit about which parts of the recommendation are engineering and which are commercial.

  • Hello world!

    Welcome to WordPress. This is your first post. Edit or delete it, then start writing!